-
Mob.:+86 186 3280 7688
-
E-mali: sales@dswirecloth.com
Mob.:+86 186 3280 7688
E-mali: sales@dswirecloth.com
Sep. 16, 2026
Why Upfront Mesh Price Alone Misleads Polymer Filtration Buyers
When a procurement manager at a plastics recycling plant in Germany or a polymer extrusion operation in South Korea sits down to compare stainless steel wire mesh suppliers, the first number on the spreadsheet is almost always unit price per square meter. It is easy to compare, easy to defend in a budget meeting, and easy to negotiate. But for extruder screen packs and polymer melt filtration components, unit price is a poor proxy for what the mesh actually costs the business over a production year. The more consequential costs hide in unplanned line stoppages, scrap rates, inventory carrying costs, and the administrative overhead of chasing documentation that never quite arrives.
Consider a hypothetical mid-sized extrusion line running 24/5. If a screen pack fails earlier than expected because of inconsistent mesh aperture or poor wire bonding, the operator must stop the line, purge the extruder, replace the screen, and restart. Each of those steps consumes labor, generates scrap polymer, and delays downstream orders. A mesh that costs a few percent less per unit but fails more frequently can easily erase its own savings in a single unplanned downtime event. This is the core reason a total cost of ownership (TCO) framework matters more than a price-per-unit comparison for polymer melt filtration and plastic recycling applications.
Most stainless steel wire mesh sold into filtration markets passes through several hands: a wire mill, a weaving shop, a fabricator, a trader, and finally the end user. Each handoff adds lead time, adds a quality inspection gap, and adds a margin. When a filtration failure occurs, responsibility is diffuse and corrective action is slow. A vertically integrated manufacturer that controls stainless steel wire drawing, weaving, and fabrication under one roof removes most of those handoffs.
For polymer filtration buyers, the operational consequences are concrete. First, delivery schedules become more reliable because production is not queued behind a third-party weaver's other customers. Second, inventory holding costs fall because buyers can order closer to consumption rather than building safety stock to cover unpredictable lead times. Third, when a specification needs adjustment—say a shift from a standard 12×64 mesh to a finer Dutch weave for a demanding melt filtration stage—the change is executed inside one production system rather than renegotiated across multiple suppliers.
Dashang Wire Mesh operates this integrated model, with in-house stainless steel wire drawing, weaving, and fabrication supporting aperture sizes from 20 microns to 20 millimeters and common specifications such as 12×64 and 24×110 mesh. For a procurement team, the relevant question is not simply whether a supplier claims integration, but whether that integration translates into shorter quoted lead times, smaller minimum order quantities on custom specifications, and a single point of accountability when something goes wrong. These are auditable claims, not marketing claims.
In polymer melt filtration, mesh quality is not binary. A screen pack can be within specification on paper and still underperform because of slight variations in wire diameter, aperture consistency, or weave tightness. Those variations show up as pressure spikes, premature screen failure, and inconsistent filtration quality—all of which generate scrap and rework downstream.
ISO9001 certification is often treated as a checkbox in supplier questionnaires. In practice, its value depends on how the quality management system is applied. A supplier that uses ISO9001 to drive incoming wire inspection, in-process weave monitoring, and final dimensional verification will produce mesh with tighter batch-to-batch consistency than a supplier that treats certification as a documentation exercise. Comprehensive test reports—covering aperture size, wire diameter, mesh count, and material grade—allow the buyer to verify consistency rather than assume it.
For a plant engineer, the practical test is straightforward: request three consecutive production lots of the same specification and compare their test reports. If the reports show tight tolerances and the physical samples perform consistently in the extruder, the quality system is doing real work. If the reports are vague or the samples vary, the certification is not delivering operational value. This is where scrap and rework costs are either controlled or quietly accumulated.
Cost Component | Typical Non-Integrated Supplier | Vertically Integrated Supplier (e.g., Dashang Wire Mesh) |
Unit mesh price | Lower headline price, but margin layered across trader and fabricator | Competitive price due to in-house wire drawing and weaving |
Unplanned downtime cost | Higher frequency due to inconsistent mesh quality and longer replacement lead times | Lower frequency due to batch consistency and faster replacement supply |
Scrap and rework | Elevated by aperture variation and premature screen failure | Reduced by ISO9001-controlled production and test report verification |
Inventory carrying cost | Higher safety stock needed to cover unpredictable lead times | Lower safety stock enabled by reliable delivery schedules |
Procurement administration | Multiple suppliers to coordinate; diffuse accountability | Single point of contact for wire, mesh, and fabricated screens |
Compliance documentation | Often incomplete or delayed; buyer chases certificates | Comprehensive documentation provided with shipment |
Operational Efficiencies from Consistent Quality and Documentation
Beyond the direct cost lines, consistent product quality and complete documentation create operational efficiencies that are harder to quantify but no less real. When mesh specifications are stable, maintenance teams can standardize screen pack changeover procedures, reduce operator training variability, and schedule preventive replacements with confidence. When documentation is complete and accurate, quality and compliance teams spend less time chasing certificates and more time on process improvement.
Regulatory pressure is also increasing. The European Commission has introduced compliance standards for industrial filtration products, including woven wire mesh, with stricter testing requirements for mesh used in chemical and food processing applications. These updates reference ISO 9044 and ASTM E2016 standards and require manufacturers to provide additional certification documentation, according to the European Commission. The policy also addresses the use of stainless steel mesh in circular economy initiatives. For polymer filtration buyers selling into European markets, supplier documentation is no longer a nice-to-have—it is a market access requirement.
Overemphasis on upfront price without operational impact analysis. If a supplier's proposal focuses entirely on unit cost and does not address downtime, scrap, or lead time, the buyer is being invited to make a partial decision.
Ignoring supplier integration and quality control in cost calculations. A TCO model that omits downtime and scrap is not a TCO model; it is a price comparison with extra steps.
Treating mesh specification as the sole decision factor. Specification matters, but two suppliers can quote the same 24×110 mesh and deliver very different operational outcomes based on weave consistency and wire quality.
Applying polymer filtration conclusions outside their context. TCO logic for extruder screens does not automatically transfer to unrelated filtration sectors or non-stainless mesh materials.
The central argument of this article is that stainless steel wire mesh for polymer melt filtration and plastic extrusion should be evaluated on total cost of ownership, not unit price alone. Vertical integration, ISO9001-controlled quality, and comprehensive documentation are not abstract credentials—they are the mechanisms that reduce downtime, scrap, inventory carrying costs, and compliance risk. The boundary condition is important: this framework applies specifically to polymer filtration and plastic extrusion applications using stainless steel woven wire mesh. It does not automatically extend to other filtration sectors or mesh materials, where different cost drivers may dominate.
For buyers who need to justify a supplier selection to finance or operations leadership, the TCO framework provides a defensible structure. It shifts the conversation from "this mesh costs less per unit" to "this supplier reduces our total filtration cost per ton of production." That is a stronger business case, and it is one that operations data can support over time.
Buyer Takeaways:
Unit price is the smallest and most visible cost component; downtime, scrap, and inventory carrying costs usually dominate the real TCO equation for polymer melt filtration.
Vertical integration in wire drawing, weaving, and fabrication improves delivery reliability and reduces procurement complexity—verify it by asking for lead times, MOQs, and a single point of accountability.
ISO9001 certification has operational value only when it drives batch consistency and test report transparency; request three consecutive lot reports and compare them.
Regulatory documentation requirements for industrial filtration are tightening, particularly in the EU; shipment-ready certification reduces compliance risk and audit exposure.
Apply this TCO framework to polymer filtration and plastic extrusion applications specifically; do not assume it transfers unchanged to other filtration sectors or mesh materials.
Need a Custom Solution?
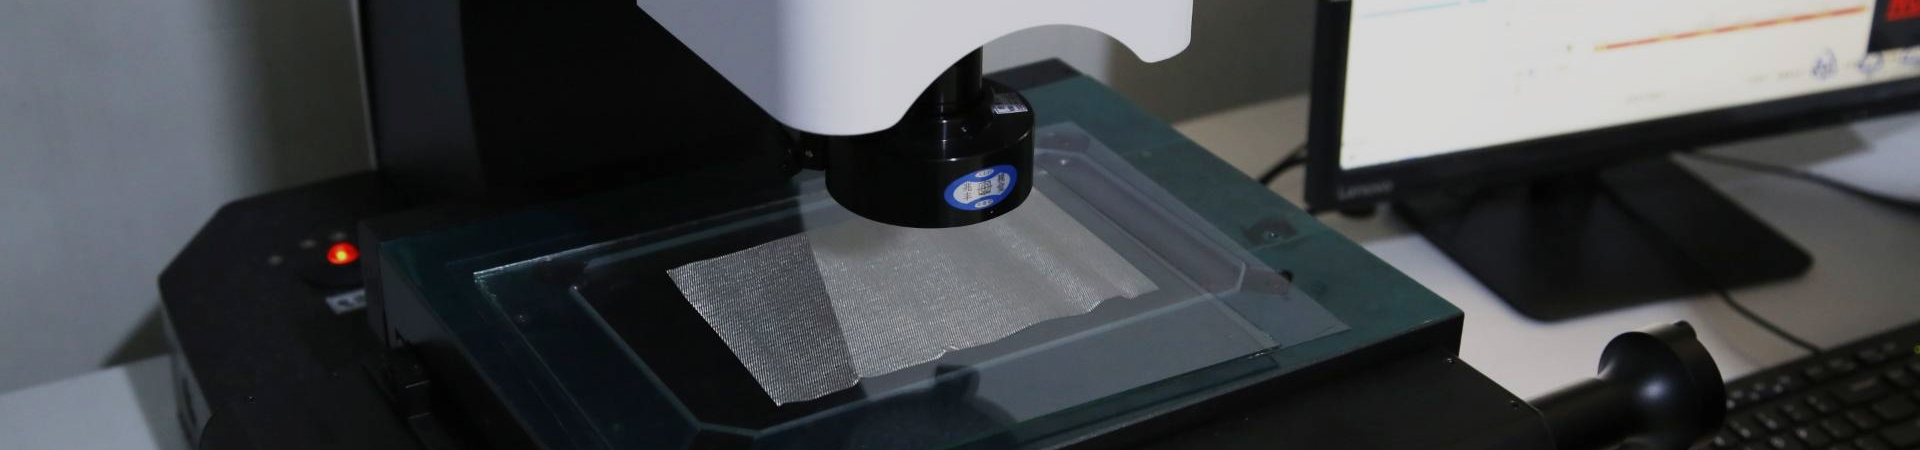
Dashang Wire Mesh has established a standard process for drawing and annealing wires, weaving mesh production and deeper processing, and inspection.
Related Products